Key Components of a Pneumatic Conveying System
The main pneumatic conveying system components are the air source, material-feeding device, conveying pipeline, air–material separator, filtration arrangement, discharge equipment and controls. They must be selected as a connected process. A suitable pump cannot compensate for an unsuitable pickup, and a receiver cannot deliver product if the downstream vessel refuses discharge.
This guide identifies each component’s role and the interfaces a buyer should check. Component selection depends on the material, route, required delivery window and receiving process; there is no universal parts list suitable for every powder.
Follow three paths through the system
Use the system scope described under UPFLOW pneumatic conveying systems as a starting point for assigning each component to the material path, air path or control sequence.
- Material: source → feeding or pickup device → conveying line → separator or receiver → discharge device → downstream process.
- Air: an air source creates the pressure difference; the air path passes through the separation and filtration arrangement appropriate to the design. The pump’s position differs between pressure and vacuum layouts.
- Control: demand and readiness signals permit feeding, transfer and discharge; level, valve and pressure information determines whether the sequence may continue.
These are functional paths, not a construction drawing. In particular, some functions share one assembly: a filter receiver may provide both air–material separation and filtration. A separate cyclone and a separate dust collector are not automatically required in every system.
Component roles and interface checks
Component choices vary across pneumatic conveying applications; record your material and receiving process before comparing equipment lists.
| Component | Function | Interface to verify |
|---|---|---|
| Air source | Establish the required pressure difference and airflow | Duty at operating conditions, air quality, connection losses and source readiness |
| Feeding or pickup device | Introduce material into the conveying stream | Source flow behaviour, feed rate, available air and pressure boundary |
| Pipeline and bends | Provide the transfer route | Actual routing, joints, wear, cleaning access and receiving location |
| Separator or receiver | Separate conveyed solids from transport air | Usable batch quantity, filter arrangement, fill endpoint and discharge clearance |
| Filtration and dust extraction | Manage the relevant air streams and retained fines | Airflow at each connection, filter condition and cleaning or maintenance access |
| Discharge and receiving equipment | Deliver material to the next process | Receiving permission, level, pressure conditions, complete emptying and weighing |
| Controls and instruments | Coordinate the agreed operating sequence | Signal ownership, valve confirmations, permissives, alarms and restart behaviour |
1. Air source: specify the duty point
Pressure systems and vacuum systems place the air source differently. Identify the intended operating arrangement before comparing blowers, vacuum pumps or compressed-air-driven equipment. Required airflow and available pressure difference must be considered together with the route and material load.
Record the air supply conditions and connection losses assumed in the quotation. If utility conditions change at the installation, the proposed operating point may also change. Air-source selection belongs in the whole-system review, not only an installed-power comparison.
2. Feeding device: separate unloading from controlled entry
Bag unloading makes material available; a pickup or feeding device introduces it into the conveying stream. Rotary valves, screws and suction pickups perform different tasks and are not interchangeable merely because each handles powder.
Confirm what happens when the source bridges, empties or is refilled. For a specific bag-fed application, use the flour bag-to-mixer interface worksheet. It separates the bag station, pickup and downstream weighing decisions.
3. Pipeline: use the real installed route
Document horizontal sections, vertical lifts, bends, flexible connections and branch points. Materials can differ in their response to impact, abrasion, moisture and residual buildup. Pipe diameter and transport conditions should be assessed for the intended duty rather than copied from an unrelated line.
Keep the route drawing aligned with the installation. A quotation based on one receiving location should not silently become a multi-destination system after purchase.
4. Separation, filtration and discharge: check the complete receiver
A receiver must separate material from conveying air and then release that material to the next process. The filter, fill control and outlet device affect whether this sequence can repeat reliably. Nominal vessel volume alone does not define usable delivered mass.
The conveying-air filter and bag-station dust extraction may serve different air streams. Identify both on the drawing. The need for any additional dust-extraction equipment should be reviewed against the actual airflow paths and site requirements.
For an existing receiving vessel, check support loads, pressure boundaries and maintenance clearance with our vacuum receiver retrofit checklist. A matching flange does not establish that the hopper can support the receiver or tolerate the proposed pressure conditions.
5. Controls: agree what happens when a component is not ready
State which controller requests material and which controller permits discharge. Add the relevant level signals, source readiness and valve confirmations to a cause-and-effect table. The equipment supplier and plant integrator should agree signal ownership and fault recovery before commissioning.
Use acceptance checks that follow material through the line: a valid request, available source, permitted transfer, confirmed receiver sequence and accepted downstream discharge. A motor-running indication alone does not prove that usable material arrived.
Diagnose the interface before replacing a component
| Observation | Interfaces to investigate | Useful record |
|---|---|---|
| Suction is present but little product arrives | Source flow, pickup air, joints and filter condition | Source level, pressure trend and discharged mass |
| Receiver fills but the process runs short | Discharge permission, retained product and refill timing | Full-cycle event log and actual delivery times |
| Weight reading changes during refill | Mechanical connections, pressure effects and stabilisation | Weight trend linked to valve and refill events |
| Product or fines appear where unexpected | Seal condition, air path, filtration and inspection findings | Photographs, batch identity and maintenance history |
These observations are investigation prompts, not a remote diagnosis. Inspect and maintain equipment under the plant’s isolation procedures; confirm a cause before changing settings or replacing parts.
Installed-project reference
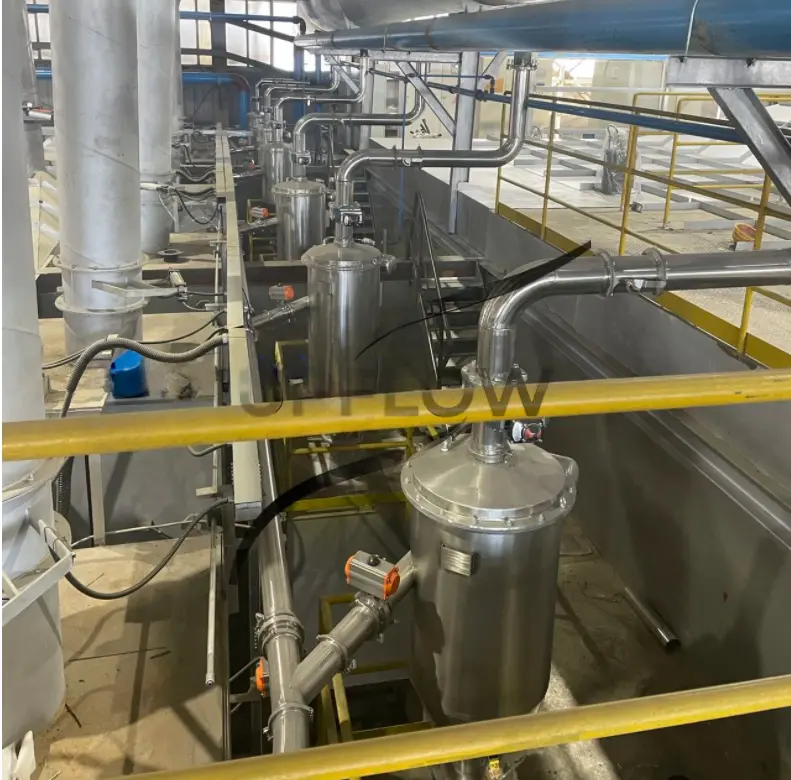
See the Korea vacuum powder-feeding project for a separate installed-project reference when discussing how feeding equipment connects to the downstream process. Its published scope does not establish performance for a different material or layout.
Watch the vacuum feeding sequence
UPFLOW’s animation below illustrates bag feeding, enclosed transfer and receivers above downstream vessels. It is a general vacuum-feeding illustration, not footage of a flour installation or a verified retrofit. Use it to discuss equipment interfaces; it does not establish capacity, food-contact suitability or the required protection design.
Watch Vacuum Feeding System on UPFLOW’s YouTube channel.
FAQ
Does every system require a rotary valve?
No. The entry and discharge devices depend on the conveying arrangement and pressure boundary. Confirm the required function before specifying a particular valve type.
Are a cyclone and a filter receiver the same component?
No. Both can participate in separation, but their operating principles and collection characteristics differ. The design may combine separation stages or use a filter receiver; review the actual air and product paths.
Which component determines capacity?
Delivered capacity depends on the complete system and operating sequence. For batch vacuum transfer, measure mass over the full conveying cycle, including discharge and process waiting.
Connect the component list to a real proposal
Complete the RFQ datasheet with material, route, delivery and interface requirements. contact UPFLOW to discuss the resulting system scope.