Tel:
+ 86 18260066893
Email:
[email protected]
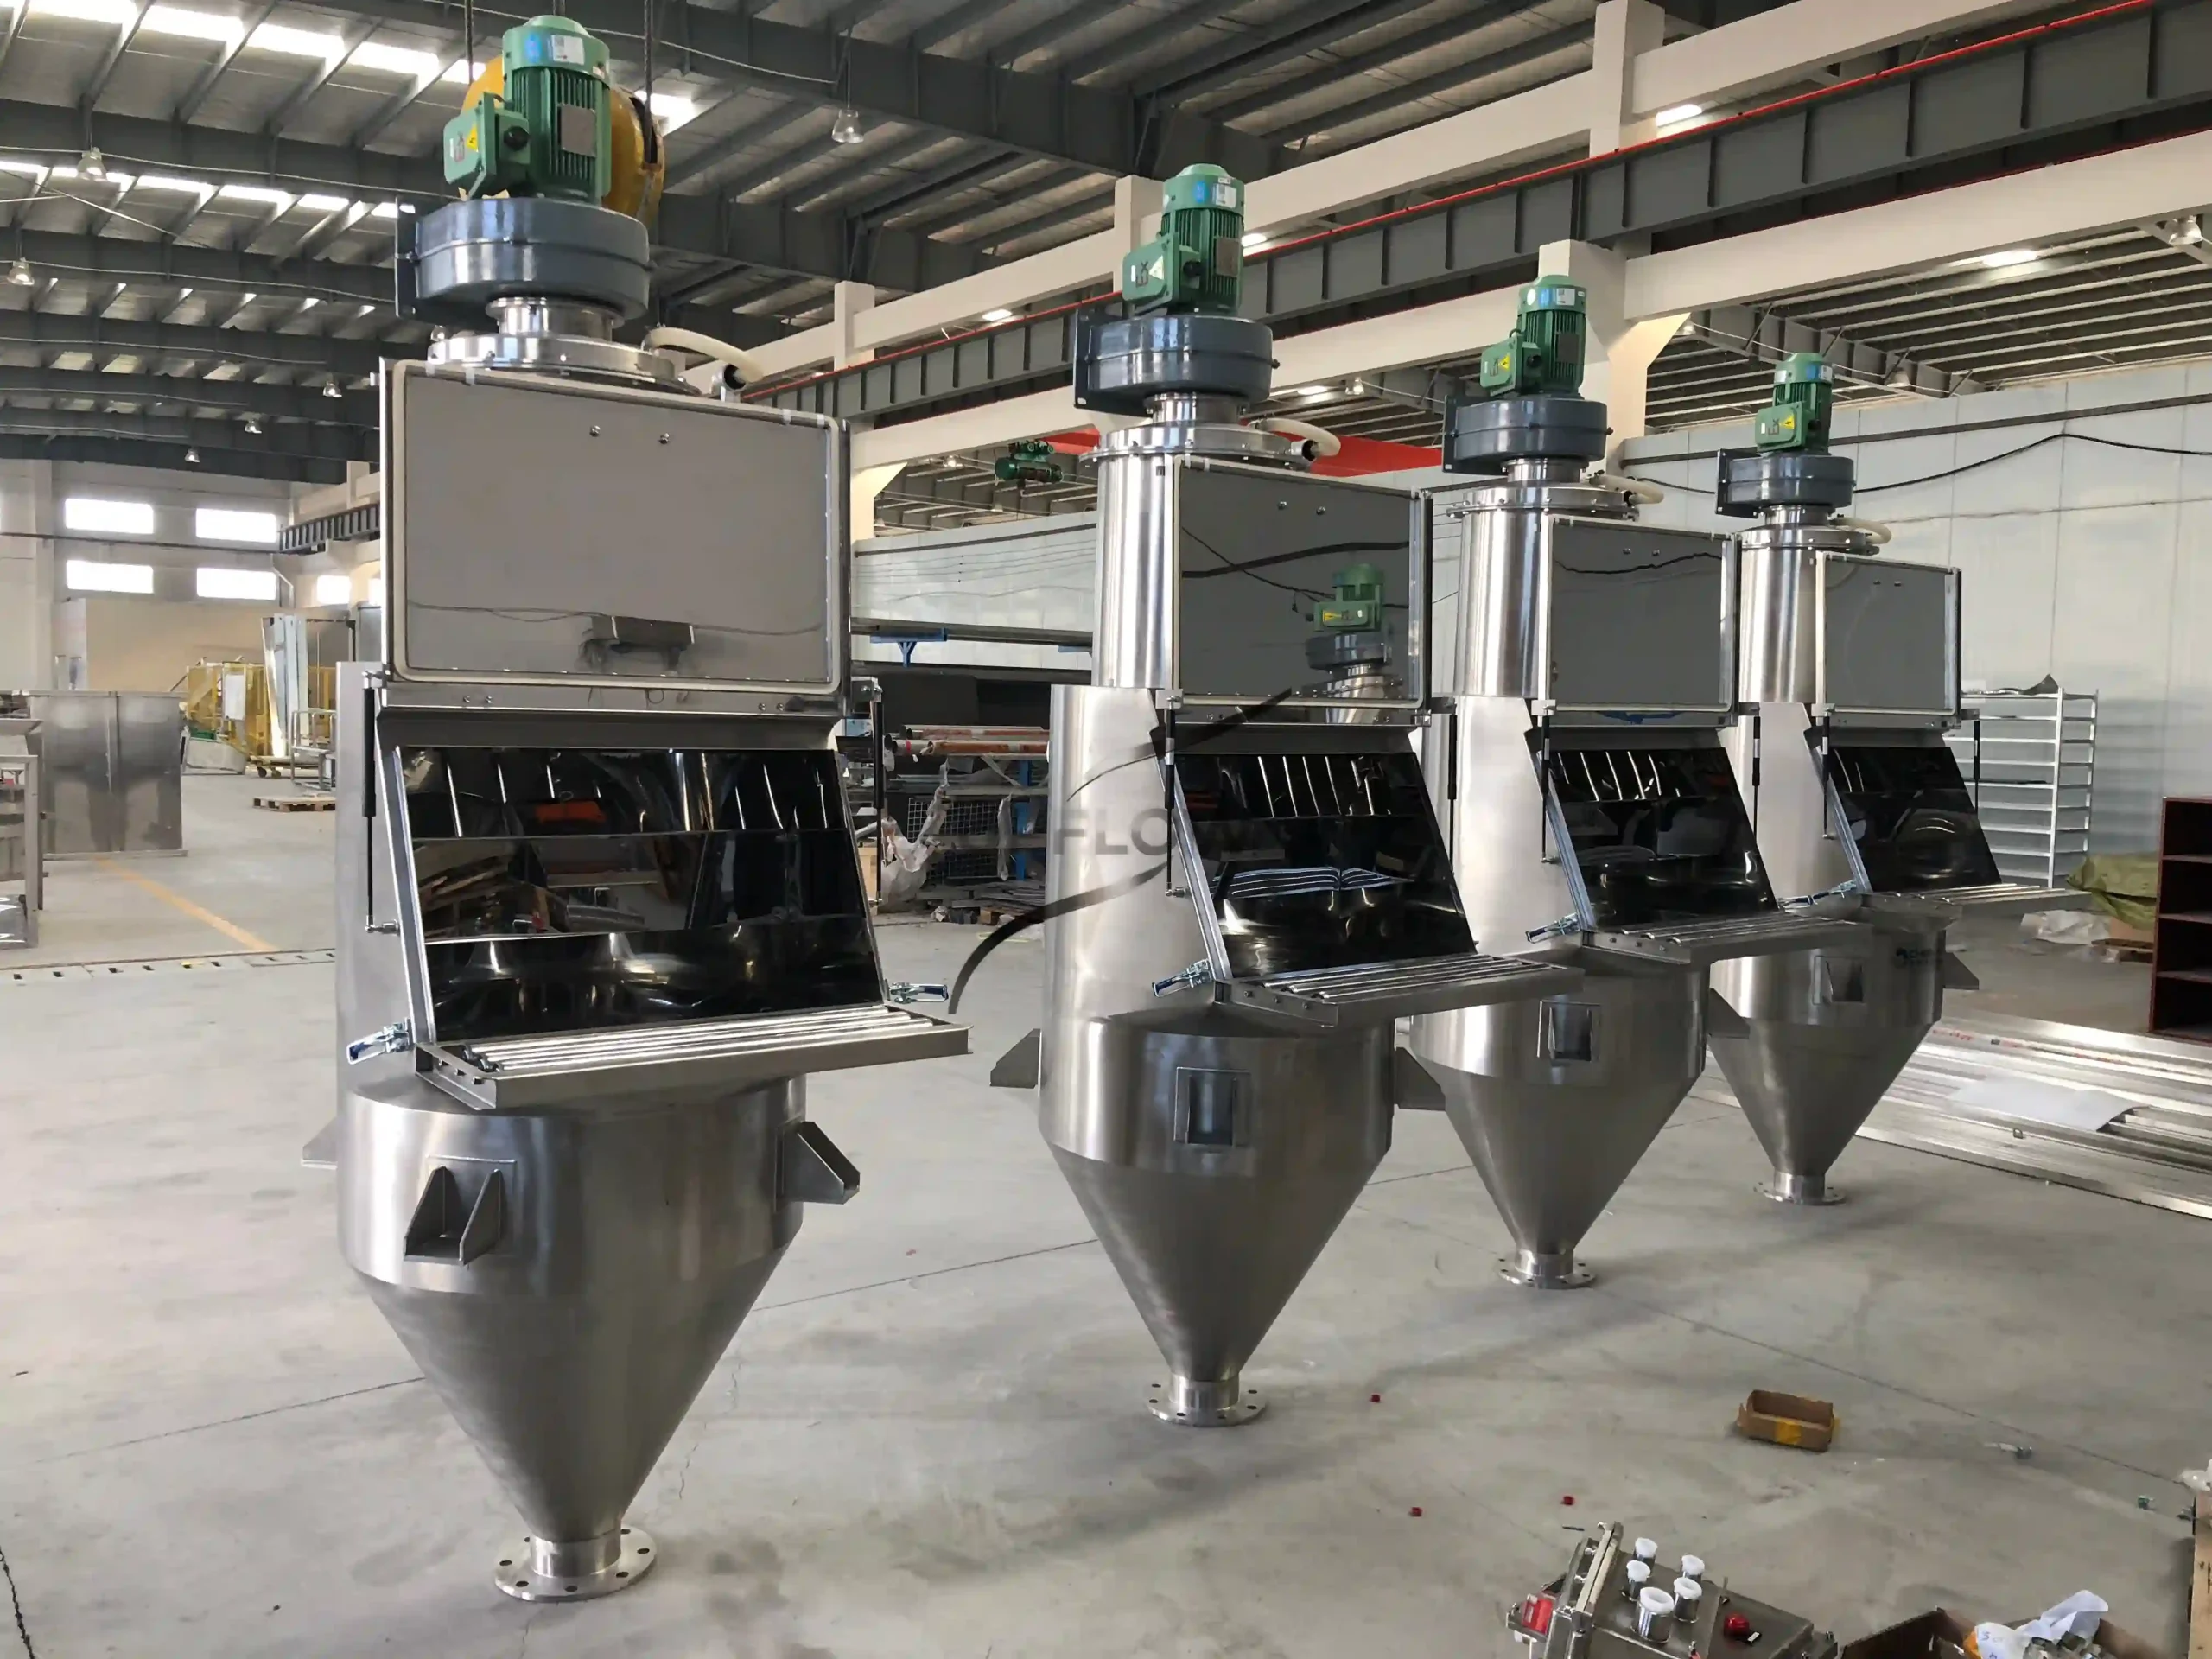
UPFLOW successfully designed and supplied a customized Vacuum Conveying System for a Korean industrial customer, providing an integrated automatic powder feeding solution designed for multiple chemical powder materials used in the customer’s production process.
Unlike standard powder transfer applications where only one material characteristic needs to be considered, this project involved several different chemical powders, including coarse oxide materials, sodium sulfate, oxalic acid and calcium hydroxide, each with different physical and chemical properties such as particle size, moisture content, acidity and alkalinity, which required a customized conveying and feeding design rather than a standard material transfer solution.
Based on the customer’s production requirements, UPFLOW developed multiple automatic powder feeding systems combining vacuum conveying technology, unpacking equipment, intermediate storage hoppers, screw feeding units, weighing systems and centralized PLC control, creating a complete enclosed powder handling process from bag opening to accurate feeding into downstream production equipment.
The Korean customer required an automated powder feeding solution to replace manual material charging operations and improve production stability, working environment and feeding accuracy.
During traditional manual powder handling processes, operators usually need to manually open bags and transfer powder into production equipment, which may result in several operational challenges, including powder dust generation, inconsistent feeding quantities, higher labor requirements and increased difficulty in maintaining a clean production environment.
Therefore, the customer required a complete automatic powder feeding system with the following functions:
Automatic bag opening and powder discharge
Dust-controlled material transfer
Stable powder feeding rate
Accurate material addition
Reduced manual operation
Easy integration with existing production equipment
To achieve these objectives, UPFLOW designed a vacuum conveying based solution capable of transporting different powders through enclosed pipelines while maintaining stable and controlled feeding performance.
The project involved multiple industrial powder materials, including:
The coarse oxide material was supplied in 25/50 kg bags, with particle size below 100 mesh, moisture content between 1% and 5%, weak water absorption characteristics and alkaline properties with a pH value between 8 and 10.
Because of its relatively coarse particle characteristics and specific feeding requirements, the system needed to maintain stable discharge performance while preventing material accumulation during transfer.
Sodium sulfate was supplied in 50 kg bags, with particle size between 50 and 100 mesh, moisture content below 1% and low water absorption characteristics.
For this type of powder, the conveying system needed to maintain reliable powder flow while ensuring accurate feeding into the production process.For more information about the sodium sulfate:Sodium Sulfate Powder Pneumatic Conveying System: Design, Performance and Industrial Applications.
Oxalic acid is a strongly acidic powder material with a pH value below 1, particle size between 50 and 100 mesh and low moisture content.
Due to its acidic characteristics, the material contact parts of the feeding system required appropriate material selection and surface treatment to improve corrosion resistance and ensure long-term equipment reliability.
Calcium hydroxide is an alkaline powder material with a pH value above 10, particle size below 100 mesh and low moisture content.
Because of its alkaline properties and fine powder characteristics, the conveying system needed to provide enclosed transportation and effective dust control during material transfer.
The main challenge of this project was not simply transporting powder materials, but developing a flexible feeding system capable of handling multiple materials with different characteristics while maintaining stable operation.
Different powders behave differently during conveying because factors such as particle size, density, moisture content, acidity and alkalinity directly influence material flow performance.
Therefore, UPFLOW considered several engineering aspects during system design, including:
Material compatibility
Contact material selection
Feeding stability
Dust control requirements
Pipeline layout
Cleaning and maintenance requirements
For chemical powder applications, the conveying system must not only achieve transportation but also protect material quality and ensure safe operation.
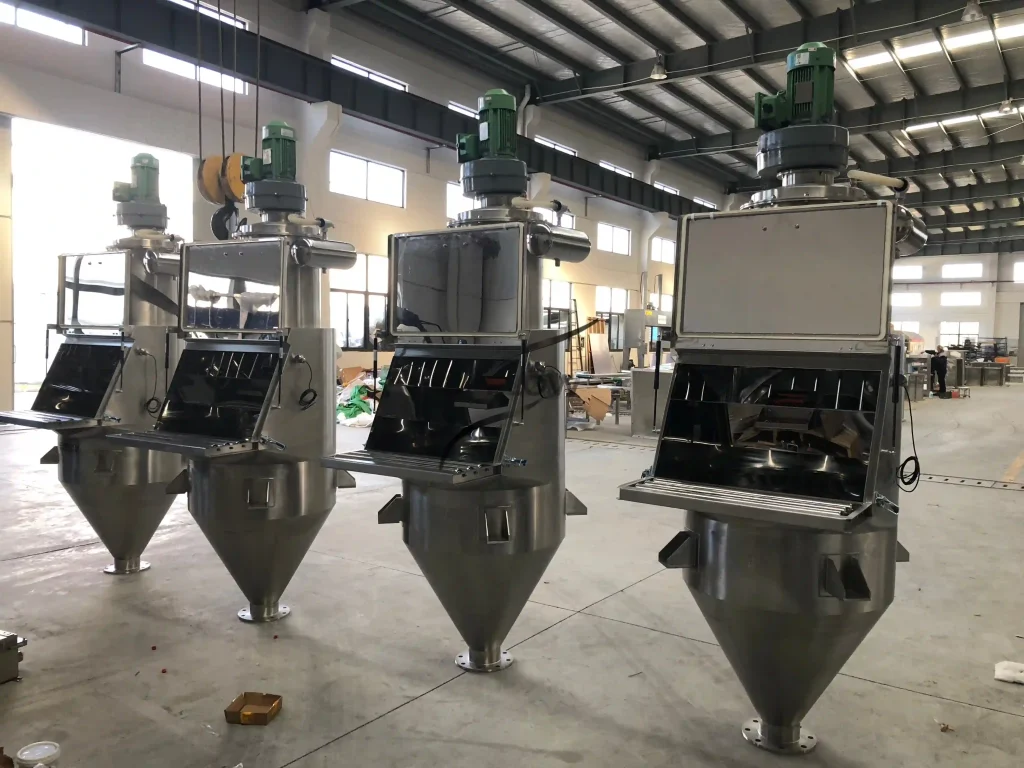
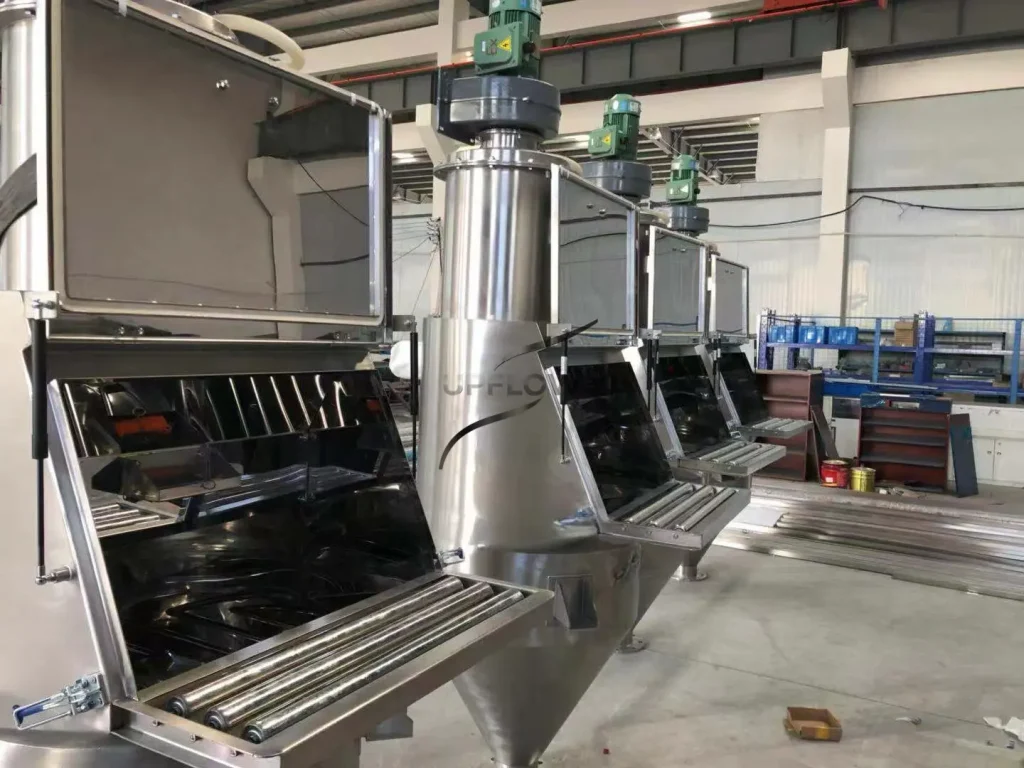
To meet the customer’s requirements, UPFLOW supplied multiple customized Vacuum Conveying Systems integrated with automatic powder feeding equipment.
The complete system included:
Dust-free bag opening machine
Vacuum conveying equipment
Intermediate transition hopper
Screw feeding machine
Weighing hopper
Conveying pipelines
PLC centralized control system
The working process starts with automatic bag opening, where powder material is discharged into the system under controlled conditions. The vacuum conveying unit then transfers the powder through enclosed pipelines into the intermediate hopper, after which the screw feeder and weighing system provide accurate material feeding according to production requirements.
This automated process significantly reduces manual intervention while improving feeding consistency and production efficiency.
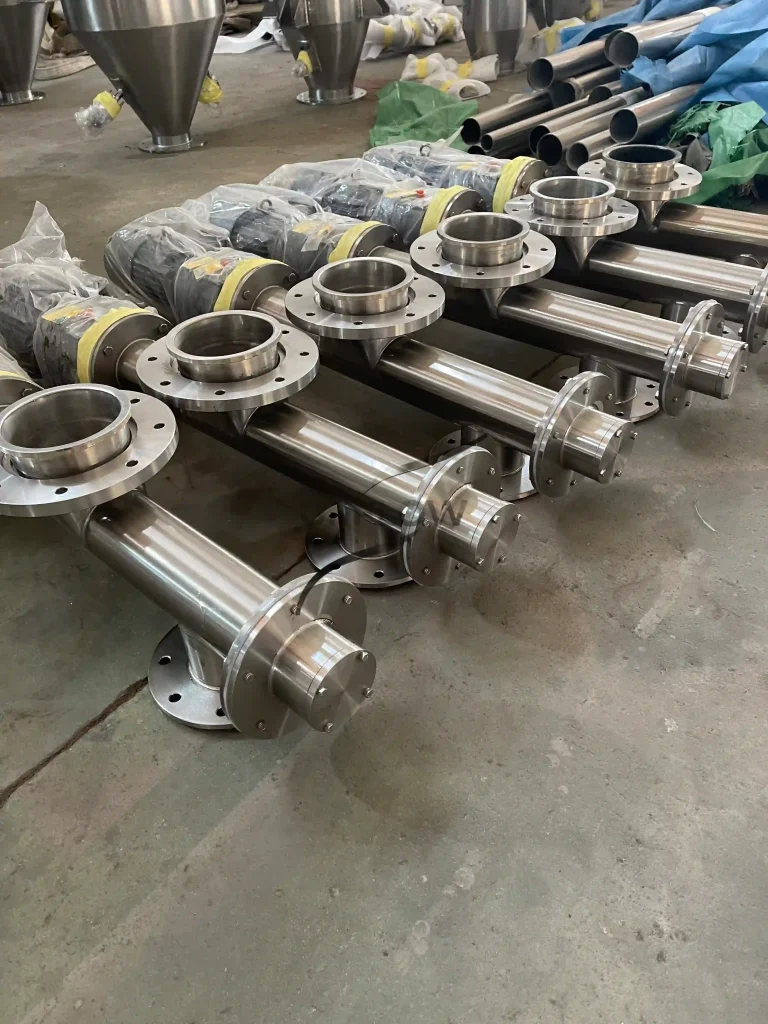
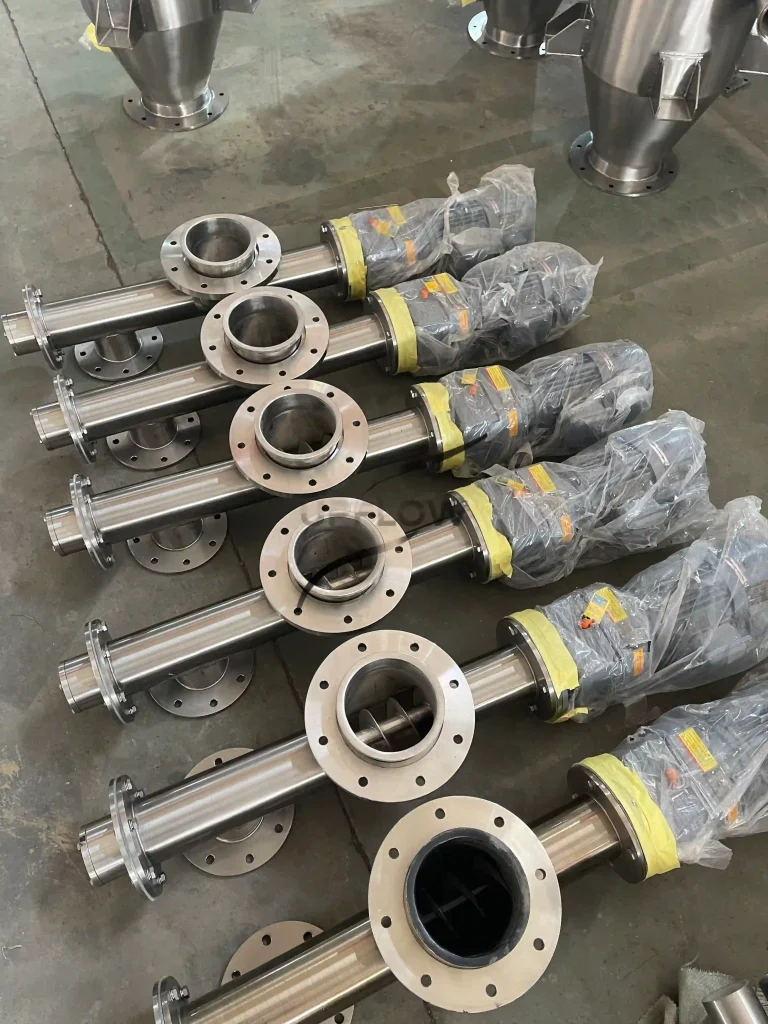
For the three automatic feeding systems handling coarse oxide material, sodium sulfate and calcium hydroxide, equipment and powder contact parts were manufactured using 304 stainless steel to provide reliable corrosion resistance and meet industrial powder handling requirements.
For the oxalic acid feeding system, the powder contact surfaces were treated with PTFE coating because of the material’s strong acidic characteristics.
This design helped improve chemical resistance and protect the equipment during long-term operation.
The complete system was integrated with Siemens PLC programming, enabling automatic operation, process monitoring and coordinated control between unloading, conveying, weighing and feeding processes.
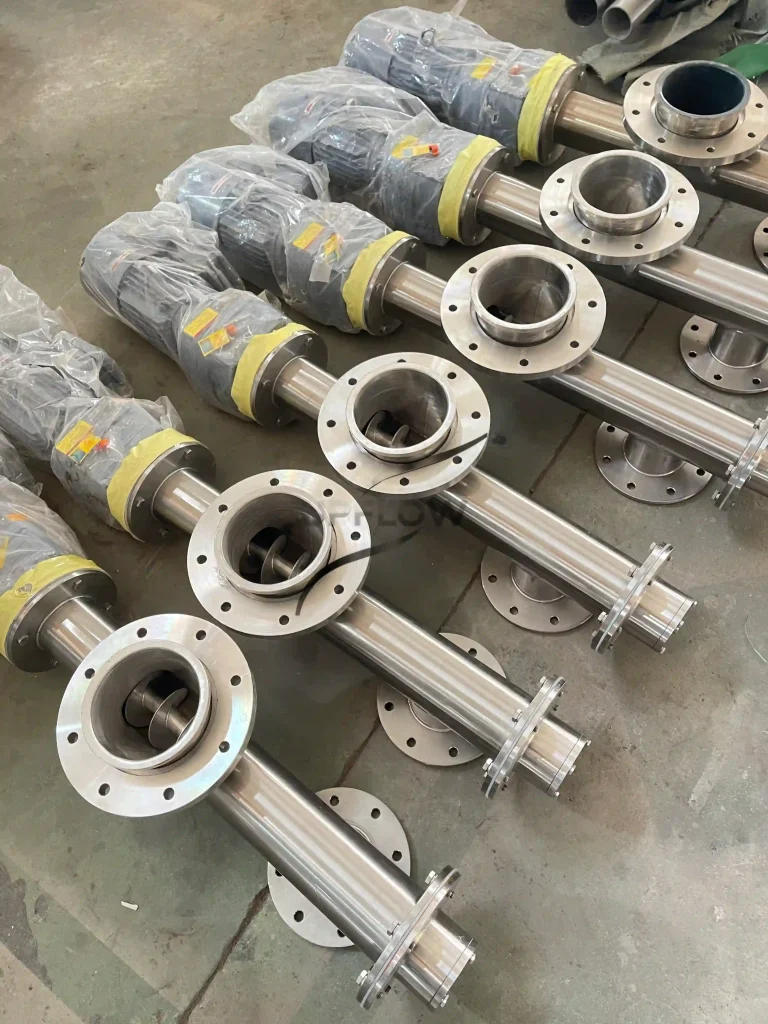
Through customized engineering design, UPFLOW successfully delivered a complete Vacuum Conveying System solution for the Korean customer.
The project achieved:
Automated powder feeding
Reduced manual material handling
Improved production consistency
Dust-controlled operation
Reliable transportation of multiple chemical powders
Customized equipment design according to material properties
This project demonstrates UPFLOW’s capability in designing customized vacuum conveying and powder feeding systems for complex industrial applications involving different powder characteristics and production requirements.
UPFLOW provides customized Vacuum Conveying Systems and automatic powder handling solutions for industries requiring clean, reliable and efficient powder transfer.
Our solutions are widely applied for:
Chemical powders
Pharmaceutical powders
Food ingredients
Battery materials
Mineral powders
Fine industrial materials
By evaluating material properties, production requirements and operating conditions, UPFLOW develops customized powder conveying systems that help customers improve automation, efficiency and process reliability.
For more project cases:
A vacuum conveying system uses negative pressure generated by a vacuum source to transport powder materials through enclosed pipelines, providing clean and efficient powder transfer.
Vacuum conveying provides enclosed transportation, reduces dust exposure and allows safer handling of fine chemical powders.
Different powders require specific engineering evaluation. UPFLOW designs conveying systems according to each material’s characteristics and production requirements.
Depending on the material characteristics, equipment can use stainless steel construction or special surface treatments such as PTFE coating for improved chemical resistance.
WhatsApp: + 86 18260066893 Email: [email protected] © 2025 All Rights Reserved by Upflowindustry.