Battery Material Pneumatic Conveying Systems: Design and Selection
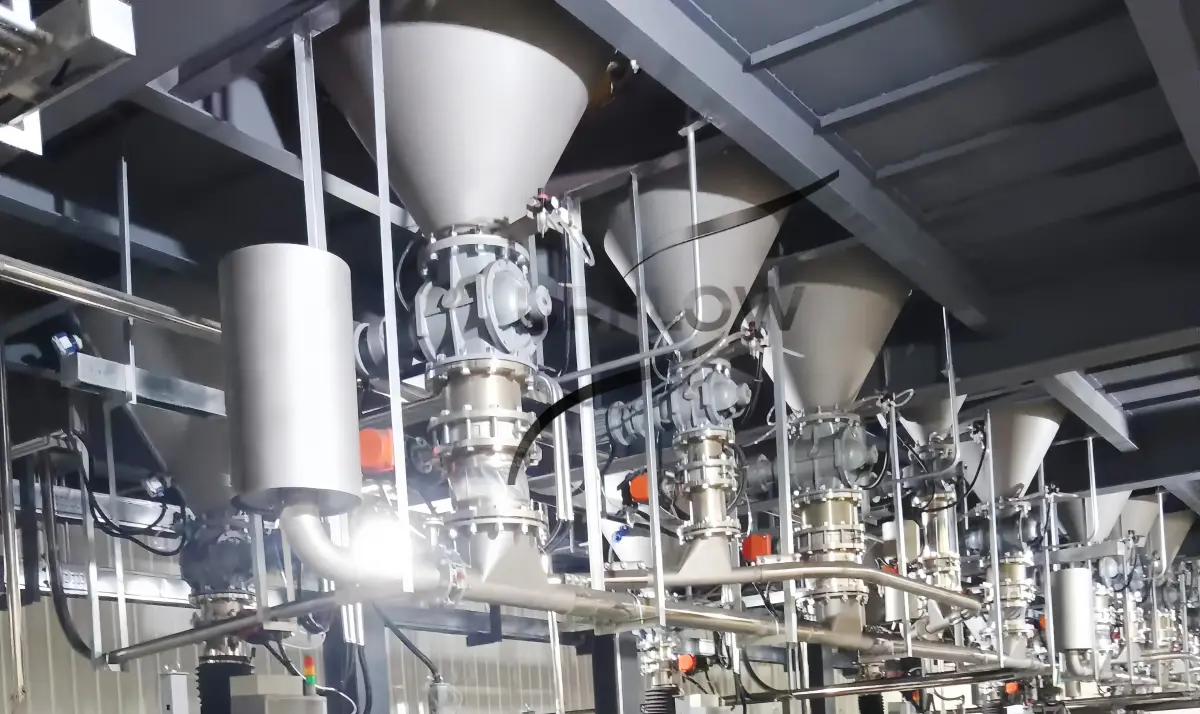
Powder-handling hoppers, valves and pipework. The final configuration must be assessed against the actual battery material and production duty.
In battery material production, pneumatic conveying transfers powders through enclosed pipelines between feeding, storage and processing equipment. A suitable system depends on the specific material, throughput, route, receiving process and product-quality requirements. A configuration selected for graphite cannot automatically be applied to a cathode powder or a binder.
For a battery production project, start by defining the transfer duty and the quality limits that must be maintained. Then evaluate feeding, conveying, filtration, discharge and controls as parts of the same process.
Which battery materials need different conveying assessments?
Battery manufacturing uses several powder groups. The table below identifies questions to resolve during engineering; it does not prescribe one conveying method for an entire group.
| Material group | Examples | Questions to establish before selection |
|---|---|---|
| Cathode-related powders | LFP, LCO and ternary cathode materials | What are the actual particle properties, contamination limits and receiving requirements? |
| Anode-related powders | Graphite and silicon-based materials | What changes in particle condition or moisture exposure are acceptable? |
| Conductive additives | Conductive carbon black and CNT-containing powders | What are the measured flow properties, feeding behaviour and filtration requirements? |
| Binder-related materials | PVDF, CMC and other specified binder powders | How do the actual grade, moisture and downstream preparation process affect transfer? |
Use the supplied grade and specification for the assessment. Two powders in the same chemical family may have different handling behaviour.
For more focused discussions, see LFP powder conveying, graphite powder conveying and conductive carbon black conveying.
Define the complete powder transfer duty
A material name and a target capacity are only the starting point. A useful design brief also states where the powder comes from, how it enters the system and what happens at the destination.
Describe the source as small bags, FIBCs, a silo or an existing hopper. Identify the receiver as a storage vessel, process hopper, mixer or another piece of equipment. Include horizontal routing, vertical lift, available headroom and connection drawings.
Set out the production schedule. Continuous demand, intermittent receiver refill and batch charging place different demands on the equipment sequence. Where one line supplies several destinations, define whether simultaneous transfer is required or sequential feeding is acceptable.
UPFLOW’s pneumatic conveying systems should be assessed against this complete duty rather than selected by the material name alone.
How should vacuum and positive pressure conveying be compared?
Compare the alternatives using the same material, route and production requirements. The choice should account for the number of feeding and receiving points, available air source, receiver interfaces, containment needs and maintenance access.
A vacuum conveying system uses a pressure below the surrounding atmosphere to draw material towards the receiver. This can support enclosed collection from a feeding point, but performance still depends on the complete system configuration and seal condition.
Positive pressure conveying introduces material into a pressurised conveying line. Feeding arrangements, receiving-vessel venting and the pressure capabilities of connected equipment need to be assessed together.
Neither approach automatically guarantees gentle transfer, low energy use or suitability for every battery powder. Conveying conditions and product acceptance criteria need to be established for the actual application.
Set measurable product-quality requirements
“Clean transfer” is too broad to serve as an acceptance criterion. Define which changes matter to the process and how they will be measured.
Relevant questions may include:
- Which material-contact surfaces and seals are acceptable?
- What contamination limits apply, and what sampling method will be used?
- What moisture exposure can the powder tolerate during transfer and waiting periods?
- Is a change in particle-size distribution relevant to the product specification?
- What residue or changeover condition must be checked before the next material?
The answers help establish the contact-material specification, access for inspection and cleaning, and any evaluation required before equipment acceptance. Do not treat stainless steel construction or an enclosed pipeline as proof that all quality requirements have been met.
Coordinate feeding, filtration, discharge and batching
Powder transfer can be restricted by the feeding or discharge stage even when the air source is operating. The system assessment therefore needs to include hopper flow, inlet feeding, receiver filtration and the downstream discharge sequence.
Discuss how filter condition will be monitored, how cleaning is managed and what happens if the receiver cannot discharge. Define material-demand signals, level detection, alarms and the permitted restart conditions with the customer’s control team.
Where recipe preparation is required, distinguish conveying from accurate dosing. The transfer stage supplies material; weighing and controlled feeding establish the batch quantity. Review the connection with the automated batching system instead of assuming that conveying rate defines dosing accuracy.
Use project experience within its actual scope
UPFLOW’s published anode material big bag unloading project documents a feeding-stage application for a European battery material manufacturer. It provides a reference for unloading and production-line integration; it should not be read as a universal performance guarantee for every battery powder.
The iron phosphate mobile conveying project describes four mobile UPFLOW-430 units. The published project specifies iron phosphate, a bulk density of approximately 0.7 t/m³ and a required transfer rate of 1–2 t/h. These are project-specific inputs, not a general capacity rating for all materials. Iron phosphate is different from lithium iron phosphate, so the project must not be presented as an LFP installation.
What should you send before requesting a proposal?
Provide the material name and grade, bulk density, particle-size information, moisture, target throughput, batch schedule, route and receiving-equipment details. Include product-quality limits, utility information and available material-specific hazard data.
For a field-by-field template, use our pneumatic conveying RFQ datasheet.
Ask for any proposed trial to have an agreed scope: the material condition, test arrangement, measurements, acceptance criteria and limitations should be clear. No configuration should be described as validated for your powder solely because a similar material has been handled elsewhere.
Frequently asked questions
Can one conveying system handle several battery powders?
It may be possible, but each material and the changeover sequence need assessment. Material compatibility, residual powder, cleaning access, receiving points and operating conditions can affect whether a shared line is appropriate.
Is vacuum conveying always the best choice for battery materials?
No. Evaluate the material, route, throughput, source and receiver arrangement, containment requirements and available utilities before choosing the system concept.
Can pneumatic conveying provide accurate battery powder batching?
It can form part of a batching process. Batch quantity and dosing performance depend on the weighing equipment, feeding arrangement, control sequence and defined acceptance conditions, as well as the material supply.
Does an enclosed system eliminate contamination and dust risks?
No. An enclosed route can help control material escape, but feeding interfaces, seals, filtration, discharge, cleaning and material-specific protective measures still require assessment.
Can a published project’s capacity be applied to my powder?
Not without reviewing the conditions. Material properties, route, feeding method and operating duty may differ. Use a project as evidence of the work performed, then define the requirements for your own application.
Discuss your battery powder handling project with UPFLOW
Send UPFLOW your battery material conveying requirements, including the powder specification, target throughput, layout and downstream process. A clear design brief helps establish the appropriate equipment scope, interfaces and next evaluation steps.