Understanding High Sensitivity Pharmaceutical Powders and Their Handling Requirements
High sensitivity pharmaceutical powders are widely used in modern pharmaceutical manufacturing, including active pharmaceutical ingredients (APIs), hormone powders, biological powders, highly potent pharmaceutical compounds and other specialized drug materials that require strict process control.
Compared with general industrial powders, high sensitivity pharmaceutical powders usually have higher requirements for cleanliness, containment, operator protection and material preservation. These powders are often characterized by fine particle size, high activity, low allowable contamination levels and strict regulatory requirements during production.
In pharmaceutical manufacturing, improper powder transfer methods may lead to several challenges, including dust emission, cross-contamination, material loss and exposure risks for operators. Therefore, a reliable High Sensitivity Pharmaceutical Powder Pneumatic Conveying System is essential for achieving safe, enclosed and controlled powder transportation.
Challenges in Handling High Sensitivity Pharmaceutical Powders
During pharmaceutical production, the transportation of sensitive powders requires more than simple material movement. The conveying system must protect both the product quality and the working environment.
Dust Control and Operator Protection
Many high sensitivity pharmaceutical powders can generate airborne particles during feeding and transfer. Open manual handling or unsuitable conveying methods may increase the risk of powder leakage and operator exposure.
A closed pharmaceutical powder handling system helps minimize dust emissions by transporting materials through sealed pipelines, creating a cleaner and safer production environment.
Contamination Prevention
Pharmaceutical powders often require extremely high purity levels because even small amounts of foreign particles may affect product quality.
A properly designed contamination-free powder conveying system reduces direct human contact and helps prevent external contamination during material transfer.
Accurate Material Transfer
Many pharmaceutical production processes require accurate feeding of powders into mixers, reactors, granulation systems or filling equipment.
Stable and controlled conveying performance is important for maintaining production consistency and reducing material waste.
What Is a High Sensitivity Pharmaceutical Powder Pneumatic Conveying System?
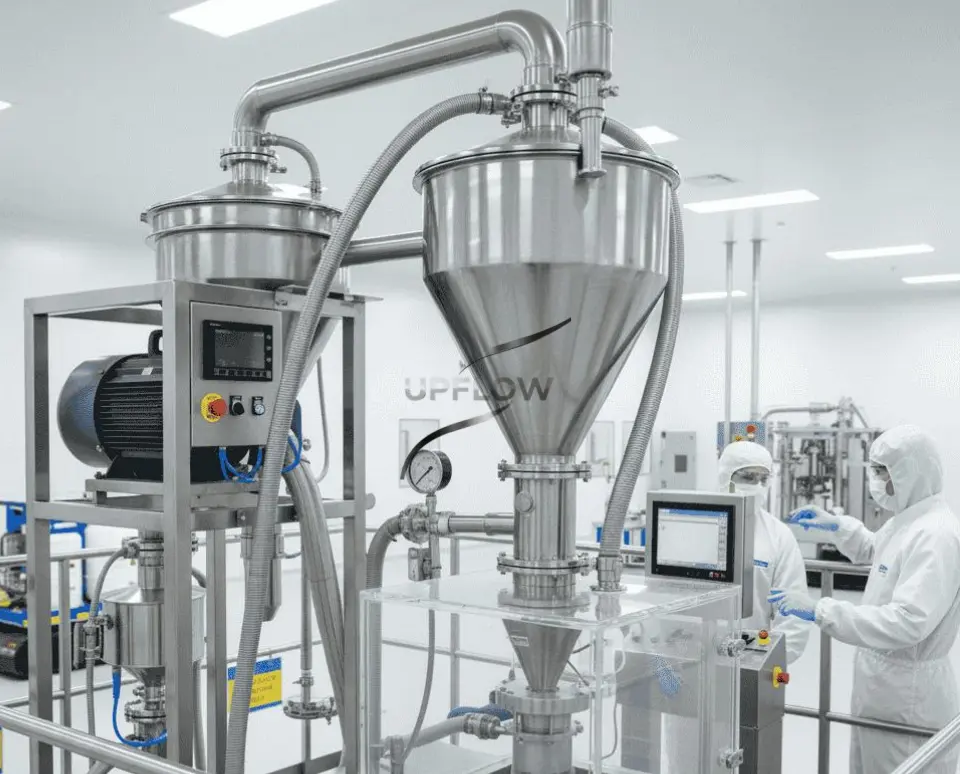
A High Sensitivity Pharmaceutical Powder Pneumatic Conveying System is an enclosed powder transportation solution that uses vacuum pressure or positive pressure airflow to move pharmaceutical powders through sealed pipelines.
Unlike traditional mechanical transfer methods, pneumatic conveying provides flexible pipeline layouts, reduced manual handling and improved cleanliness for sensitive pharmaceutical applications.
Depending on production requirements, the system can also be designed as:
GMP powder transfer system
vacuum conveying system for pharmaceutical powders
pharmaceutical powder feeding system
enclosed powder transportation system
The final system configuration depends on factors such as powder characteristics, conveying distance, production capacity and pharmaceutical process requirements.
How Does a Pneumatic Conveying System Handle Sensitive Pharmaceutical Powders?
A pharmaceutical pneumatic conveying system works by creating controlled airflow inside a closed pipeline.
For sensitive pharmaceutical powder applications, vacuum conveying is often preferred because the system operates under negative pressure, helping prevent powder leakage into the surrounding environment.
During operation:
1.Pharmaceutical powder is loaded into the feeding equipment.
2.Vacuum pressure transports the powder through sealed pipelines.
3.Filters separate powder particles from conveying air.
4.The material is discharged into the next production stage.
This enclosed conveying process helps maintain product quality while reducing dust generation and contamination risks.
Key Design Considerations for Pharmaceutical Powder Conveying Systems
Designing a High Sensitivity Pharmaceutical Powder Pneumatic Conveying System requires detailed evaluation of both material properties and production conditions.
Hygienic Equipment Design
Pharmaceutical applications usually require smooth internal surfaces, easy cleaning and suitable construction materials to meet hygiene requirements.
Stainless steel equipment design is commonly selected for pharmaceutical powder handling applications.
Powder Characteristics Evaluation
Before designing the conveying system, engineers need to consider:
Particle size
Bulk density
Flowability
Moisture sensitivity
Material activity
Required conveying capacity
Different pharmaceutical powders may require different conveying methods and operating parameters.
Integration with Pharmaceutical Production Lines
A complete powder handling solution may include:
Bag dumping stations
Vacuum conveyors
Storage vessels
Feeding systems
Weighing and batching equipment
This allows pharmaceutical manufacturers to achieve automated and consistent material transfer.
Advantages of High Sensitivity Pharmaceutical Powder Pneumatic Conveying Systems
A well-designed High Sensitivity Pharmaceutical Powder Pneumatic Conveying System provides several benefits for pharmaceutical manufacturers.
Enclosed and Dust-Free Operation
The sealed conveying process reduces powder exposure and improves workplace cleanliness.
Reduced Contamination Risk
Closed transportation minimizes human contact and helps protect pharmaceutical material purity.
Flexible Installation
Pneumatic conveying pipelines can be arranged according to factory layouts, making them suitable for complex production environments.
Automated Powder Transfer
The system can be integrated with feeding, weighing and batching processes to improve production efficiency.
Applications of Pharmaceutical Powder Pneumatic Conveying Systems
High sensitivity pharmaceutical powder conveying systems are commonly used in:
API powder handling
Hormone powder transfer
Biological pharmaceutical production
Vaccine-related material processing
Pharmaceutical excipient handling
Capsule filling powder feeding
Tablet production processes
By providing controlled and enclosed powder transportation, pneumatic conveying technology supports modern pharmaceutical manufacturing requirements.
UPFLOW Solution for High Sensitivity Pharmaceutical Powder Handling
UPFLOW provides customized High Sensitivity Pharmaceutical Powder Pneumatic Conveying Systems for pharmaceutical manufacturers requiring safe, clean and reliable powder transfer solutions.
Similar pharmaceutical powder handling challenges can also be found in API powders, hormone powders and plant extract powders, where contamination control and enclosed transfer are critical. For more API powder handling news: API Powder Pneumatic Conveying System for High-Containment Pharmaceutical Powder Handling.
Our engineering team evaluates each project according to:
Material characteristics
Production capacity
Conveying distance
Factory layout
Process requirements
Based on these factors, UPFLOW can provide customized solutions including vacuum conveying systems, powder feeding systems, batching systems and integrated powder handling equipment.
With experience in industrial powder handling applications, UPFLOW helps customers improve production automation, reduce manual operation and achieve more reliable pharmaceutical powder transportation.
FAQ
What is a high sensitivity pharmaceutical powder?
High sensitivity pharmaceutical powders are pharmaceutical materials requiring strict control of contamination, exposure and handling conditions, including APIs, biological powders and highly active compounds.
Why is pneumatic conveying suitable for pharmaceutical powders?
Pneumatic conveying provides enclosed transportation, reduces dust generation and allows flexible integration with pharmaceutical production equipment.
Is vacuum conveying suitable for sensitive pharmaceutical powders?
Yes. Vacuum conveying is commonly used for sensitive powders because it helps prevent powder leakage and supports cleaner material transfer.
Can pharmaceutical powder conveying systems be customized?
Yes. Pneumatic conveying systems can be designed according to powder properties, production capacity and pharmaceutical process requirements.